Our History
1. Production
At Hacienda Ortigosa, we have an annual production of 300,000 liters of monovarietal
Arbequina extra virgin olive oil, and a storage capacity of
1,200,000 liters in our cellar. Our estate spans over
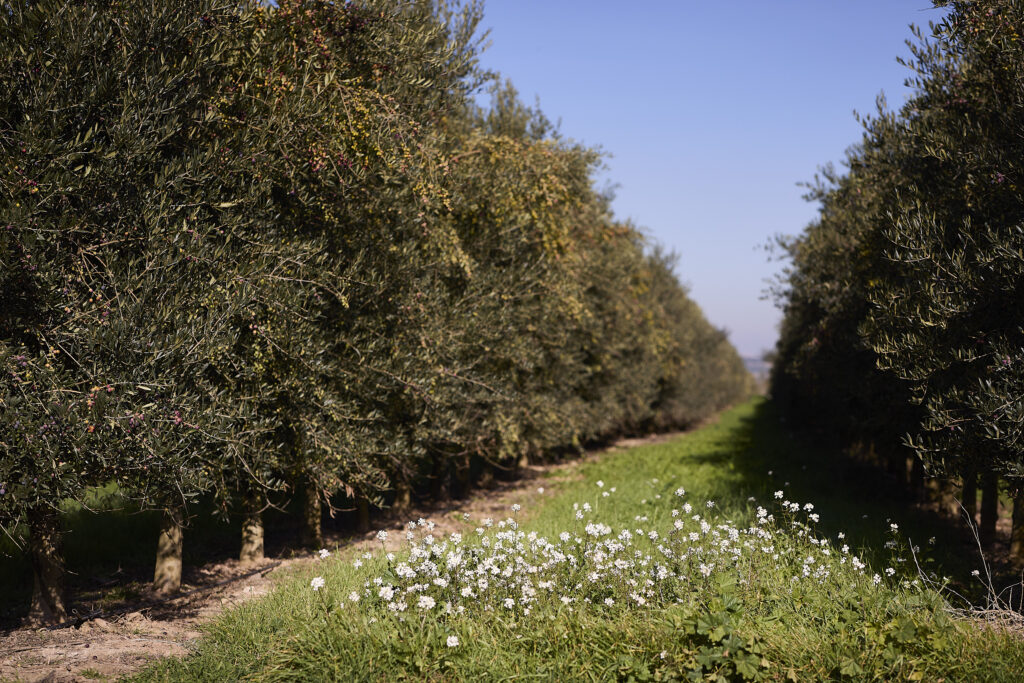
270 hectares, with more than 350,000 olive trees, machinery sheds, and all the
recursos necesarios para garantizar un aceite de la más alta calidad.
2. Optimal Harvesting
The quality of our oil begins in the field. Prioritizing fruit excellence means sacrificing yield: we harvest olives at their optimal, early stage of ripeness to obtain an oil with greater aroma, intense flavor, and exceptional properties.
3. Irrigation and Olive Grove Care
We have a drip irrigation system that allows for controlled fertilization and electronic monitoring of each sector of the olive grove. Any anomaly is detected immediately, ensuring optimal care of the olive trees.
4. Process Control and Autonomy
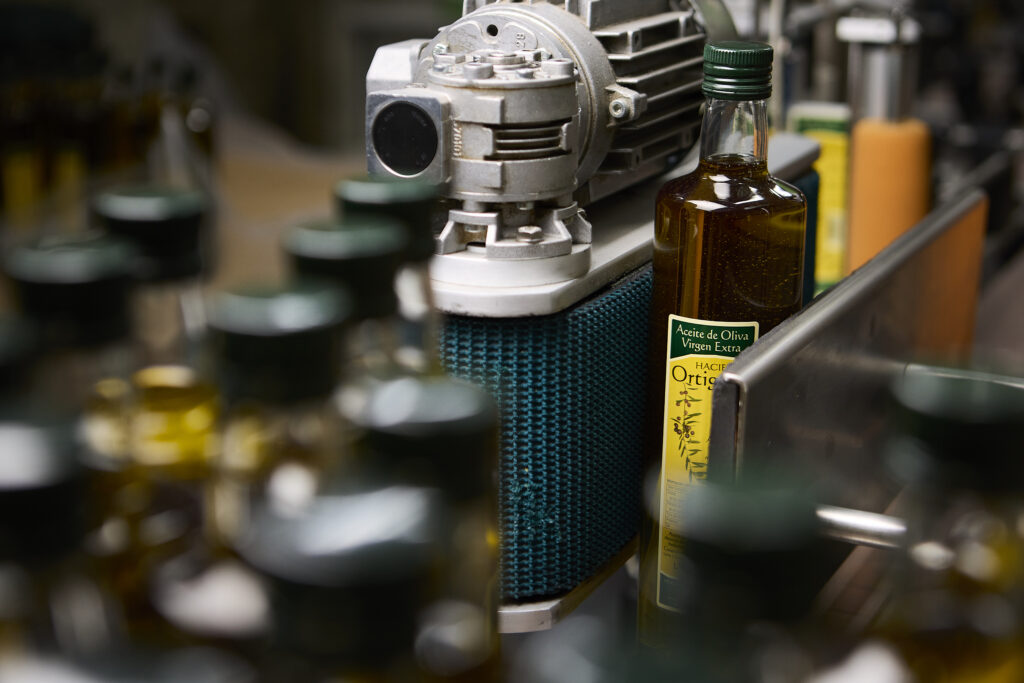
We are autonomous in all phases of production: we harvest, transport,
mill, extract, store, and bottle our oil using
our own resources. This autonomy provides us with flexibility, speed, and total control
over the quality of our product, allowing us to respond agilely to our
customers.
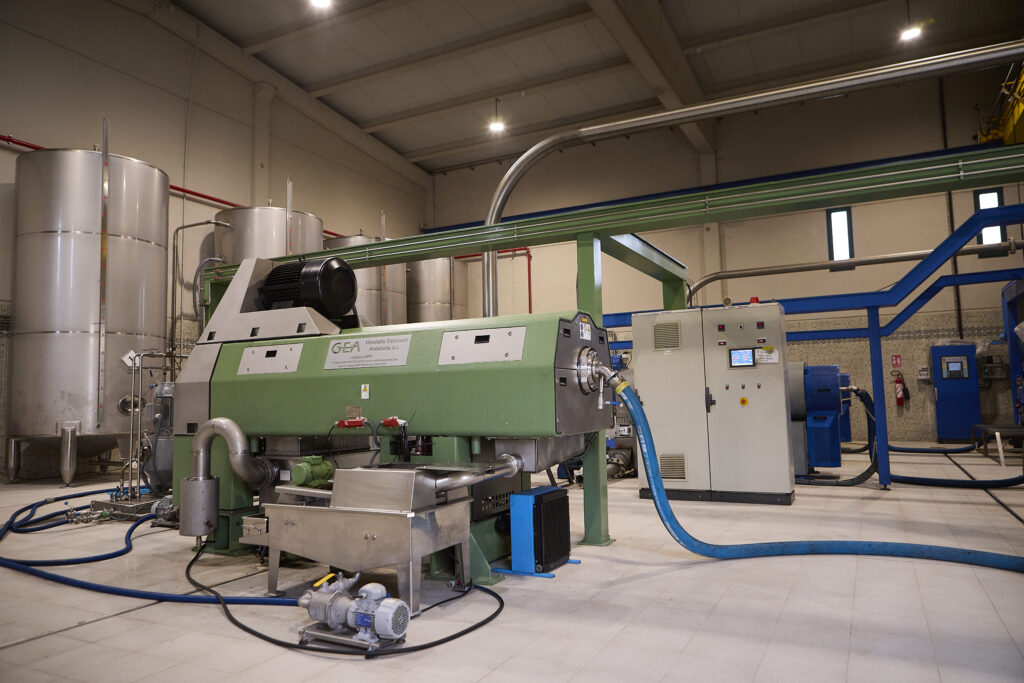
5. Manufacturing and High Technology
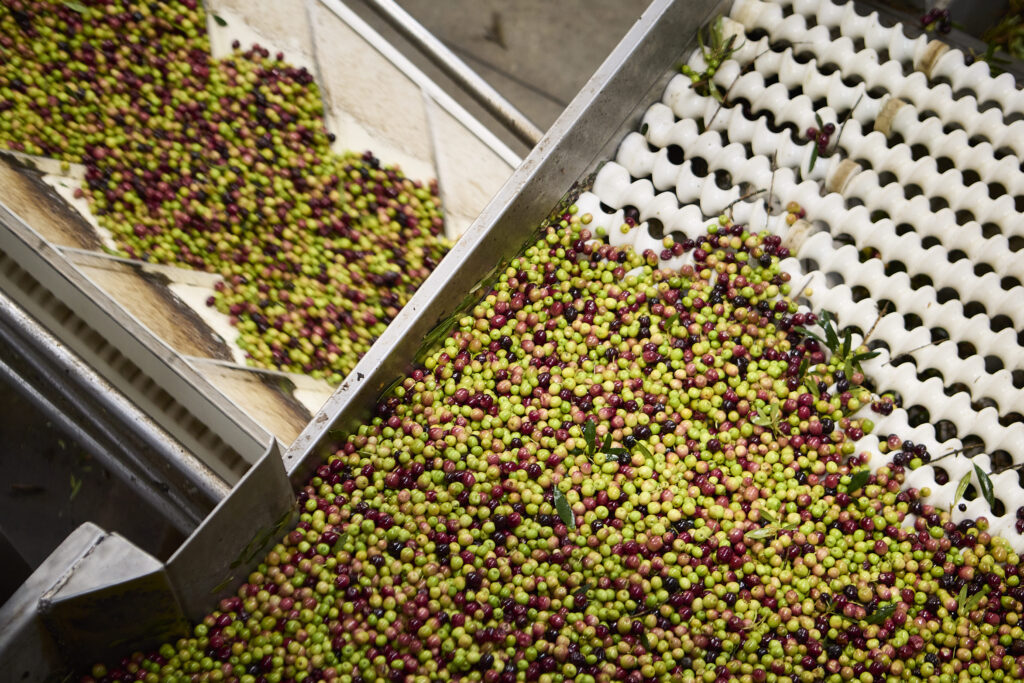
The proximity of the olive groves to the oil mill, along with high-capacity machinery and advanced technology, reduces the time from harvesting to oil extraction to less than 12 hours. This prevents olive oxidation and preserves all their organoleptic properties, guaranteeing the unmistakable flavor and aroma of our oil.
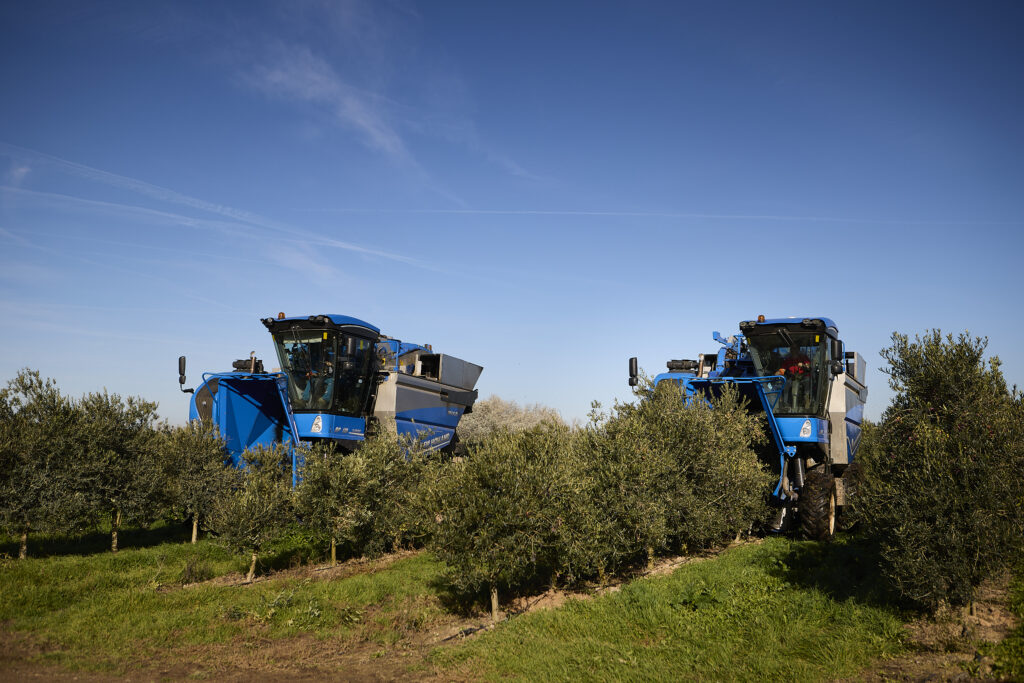
We have state-of-the-art harvesting machines, tools for field care, transport vehicles for olives, extraction machinery, a climate-controlled cellar, and inerted tanks, all designed to obtain the highest quality extra virgin olive oil.
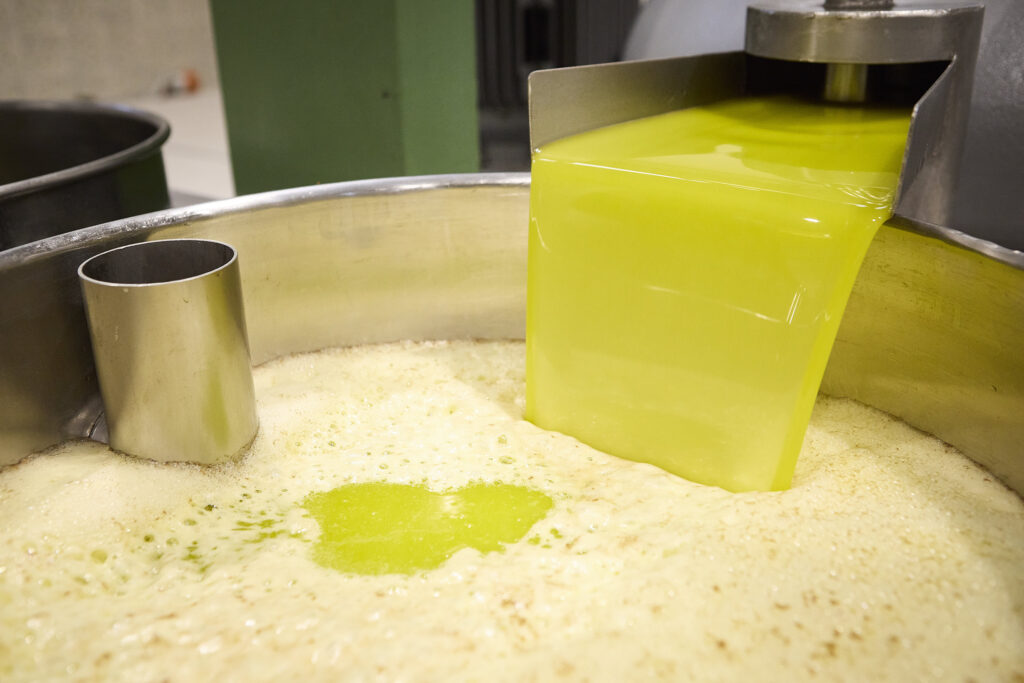
6. Cold Extraction
Our extra virgin olive oil is cold-extracted at a maximum temperature of 27°C, which preserves all the natural properties of the olive and gives the oil a unique flavor, aroma, and appearance.
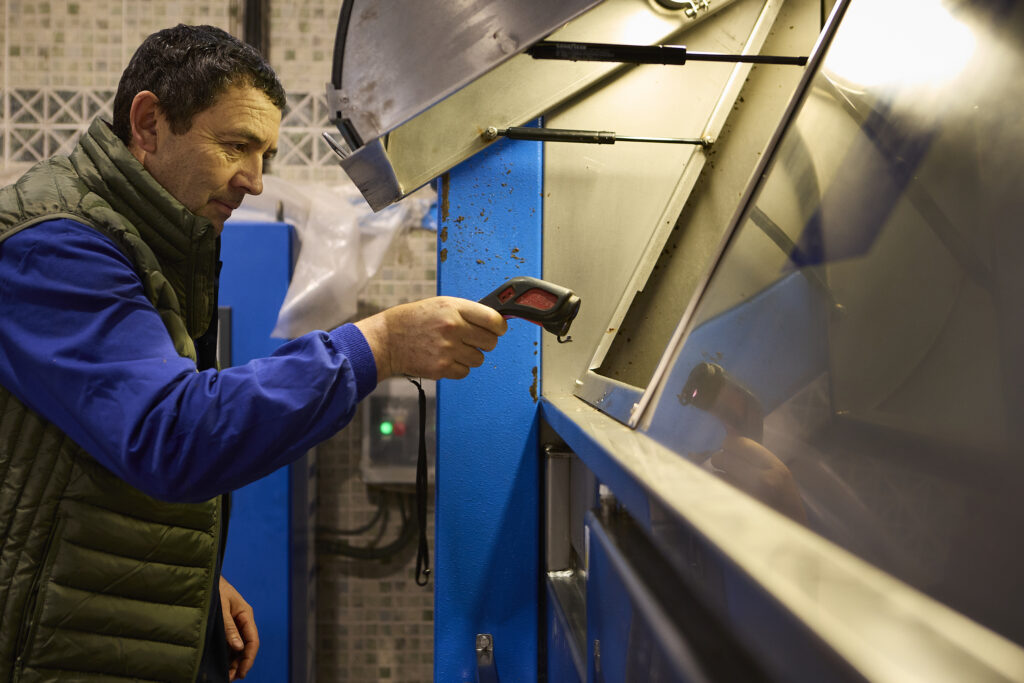
7. Quality Control
We carry out rigorous controls at all production stages, supported by our
laboratory. We analyze the acidity, fat yield, and moisture content of the
olives, ensuring that each batch meets the highest standards before reaching
the consumer.
8. Circular Economy
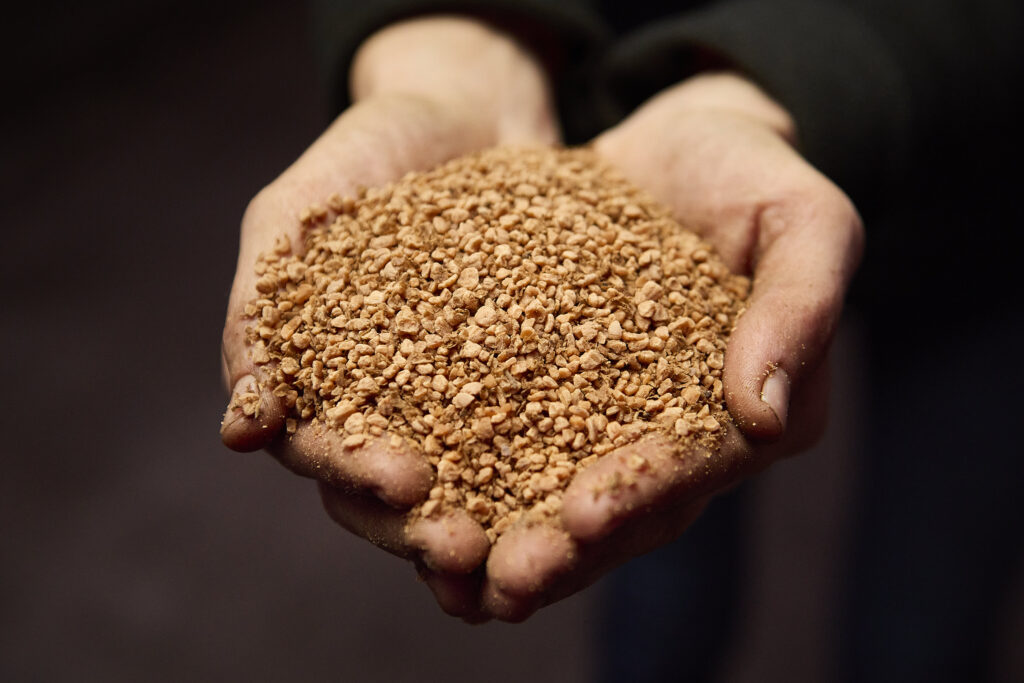
We give a second life to the olive pits generated during our production process:
• As a natural ingredient in our exfoliating products.
• As a source of renewable energy (biomass), which allows us to generate heating and hot water in our facilities.
In this way, we close the production cycle, reduce waste, and create added value from available resources.
1. Production
At Hacienda Ortigosa, we have an annual production of 300,000 liters of monovarietal Arbequina extra virgin olive oil, and a storage capacity of 1,200,000 liters in our cellar. Our estate spans over 270 hectares, with more than 350,000 olive trees, machinery sheds, and all the necessary resources to guarantee the highest quality oil.
2. Optimal Harvesting
The quality of our oil begins in the field. Prioritizing fruit excellence means sacrificing yield: we harvest olives at their optimal, early stage of ripeness to obtain an oil with greater aroma, intense flavor, and exceptional properties.
3. Irrigation and Olive Grove Care
We have a drip irrigation system that allows for controlled fertilization and electronic monitoring of each sector of the olive grove. Any anomaly is detected immediately, ensuring optimal care of the olive trees.
4. Process Control and Autonomy
We are autonomous in all phases of production: we harvest, transport, mill, extract, store, and bottle our oil using
our own resources. This autonomy provides us with flexibility, speed, and total control over the quality of our product, allowing us to respond agilely to our customers.
5. Manufacturing and High Technology
The proximity of the olive groves to the oil mill, along with high-capacity machinery and advanced technology, reduces the time from harvesting to oil extraction to less than 12 hours. This prevents olive oxidation and preserves all their organoleptic properties, guaranteeing the unmistakable flavor and aroma of our oil.
We have state-of-the-art harvesting machines, tools for field care, transport vehicles for olives, extraction machinery, a climate-controlled cellar, and inerted tanks, all designed to obtain the highest quality extra virgin olive oil.
6. Cold Extraction
Our extra virgin olive oil is cold-extracted at a maximum temperature of 27°C, which preserves all the natural properties of the olive and gives the oil a unique flavor, aroma, and appearance.
7. Quality Control
We carry out rigorous controls at all production stages, supported by our laboratory. We analyze the acidity, fat yield, and moisture content of the olives, ensuring that each batch meets the highest standards before reaching the consumer.
8. Circular Economy
We give a second life to the olive pits generated during our production process:
• As a natural ingredient in our exfoliating products.
• As a source of renewable energy (biomass), which allows us to generate heating and hot water in our facilities.
In this way, we close the production cycle, reduce waste, and create added value from available resources.

John Doe
Coffee Lover
Jack Ammar
Security
Lopez Jota
Driver